FRP Scrubbers and Ductwork for Acid Fume Control
A manufacturer's perspective on FRP scrubbers and ductwork for acid fume control — condensate chemistry, resin and liner selection, the vacuum design case, and the ASTM standards we build and verify to.
FRP Scrubbers and Ductwork for Acid Fume Control: A Manufacturer's Perspective
A wet scrubber is the one piece of equipment in a plant that is deliberately fed the worst thing the process produces. Everything else handles a controlled stream; the fume control system handles whatever escapes. It sees acid mist, saturated vapor, temperature swings, carryover droplets, and condensate that forms and re-forms on every interior surface.
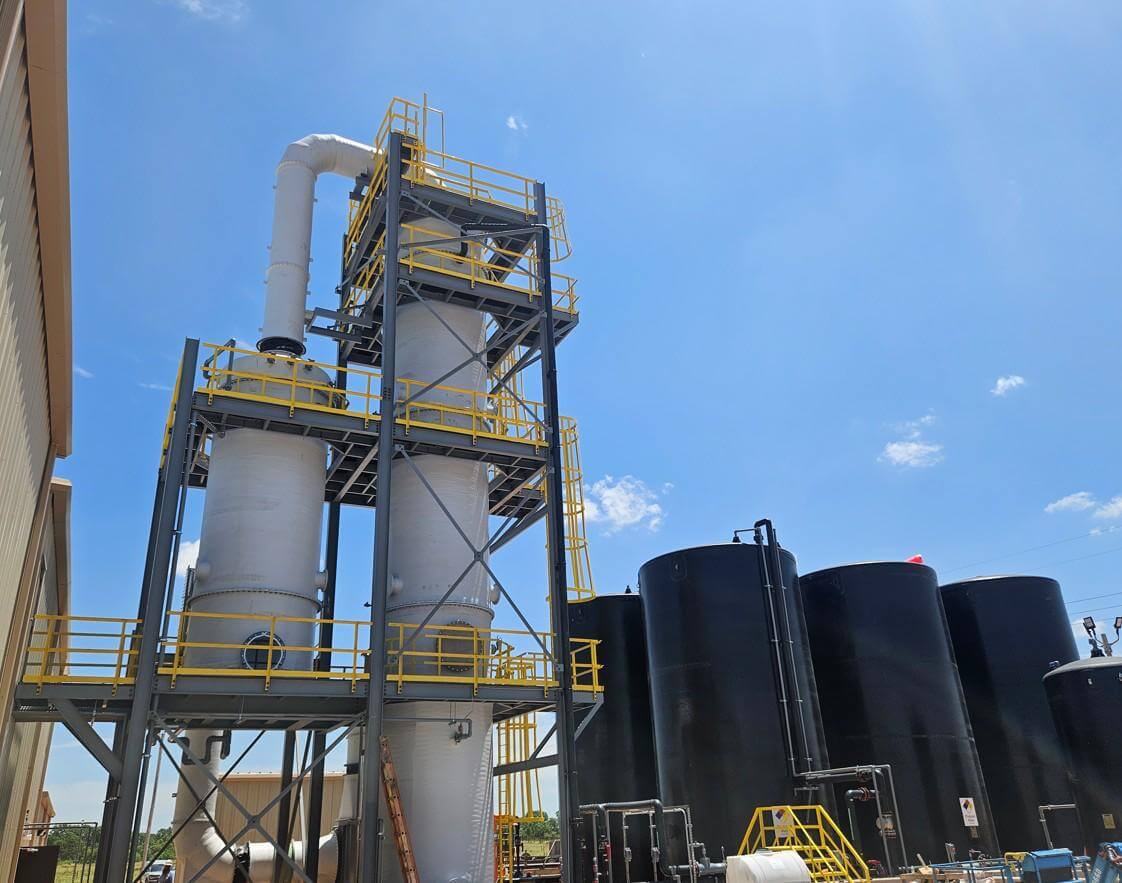
At Plastimarmol we have been fabricating FRP scrubbers, ductwork, hoods, transitions, and stacks for more than four decades. This article explains how we design and build that equipment, what information we need from the client before the first ply is laid, and the ASTM standards we build and verify to.
The Gas Stream Is Not the Problem — the Condensate Is
Most specifications we receive describe the duty by naming the gas: hydrochloric acid fumes, sulfuric acid mist, chlorine, sulfur dioxide, nitric fumes from a pickling line. But dry gas at temperature is rarely what destroys the equipment. What destroys it is the liquid phase that condenses on the wall of the duct or on the shell of the absorber.
That condensate is not the same chemistry as the scrubbing liquor. It is typically far more concentrated, it sits as a thin film against the laminate for long periods, and it concentrates further as the equipment cycles between operation and idle. A duct handling a modest fume concentration can develop wall condensate aggressive enough to attack a resin system that would handle the bulk liquid without difficulty.
For that reason, when we quote, we select the corrosion barrier for the condensate and not for the average gas composition. Where the condensate chemistry is unknown, we need the dew point, the normal and upset gas temperatures, and the concentration range of each acid species so the resin can be chosen against a realistic worst case.
A Fume Control System Is Not One Laminate
A complete fume control train has several zones, and they do not all see the same duty:
- Collection hoods and inlet ductwork. The hottest, driest section. Temperature governs here, not chemistry.
- Quench or dilution section. Where hot gas meets liquid. Thermal shock, erosion, and the steepest temperature gradient in the system.
- Absorber shell and packing support. Fully wetted, continuous liquid contact, plus the dead weight of packing and hold-up liquid.
- Mist eliminator and outlet duct. Saturated gas and a permanent condensate film. Usually the most frequent failure point, because it is the least inspected.
- Stack. Wind load, thermal cycling, UV exposure, and condensate running back down the inside wall.
We fabricate FRP for all of these zones, but not with the same laminate. A specification calling for a single laminate schedule across the whole system is either over-building the dry sections or under-building the wetted ones. Our proposals break the laminate schedule out by zone, and we recommend the client review it that way.
Resin Selection: Temperature First, Chemistry Second
In an atmospheric tank the chemistry is known and stable and the temperature is usually modest. In a scrubber, temperature is the variable that most often turns out to be higher than the user assumed.
Standard vinyl ester laminates are suitable for continuous service in the range of roughly 180–200°F (82–93°C). Above that, the options are to cool the gas before it enters the FRP section, to move to a higher-temperature resin system, or to protect the laminate with a thermoplastic or fluoropolymer liner bonded to the FRP structural wall.
Where a fluoropolymer liner is warranted, the choice is driven by the required continuous service temperature. Published continuous service ranges for the common liner materials are:
- PFA: −310°F to 500°F (−190°C to 260°C)
- MFA: −310°F to 482°F (−190°C to 250°C)
- FEP: −310°F to 401°F (−190°C to 205°C)
- ECTFE: −105°F to 320°F (−76°C to 160°C)
- ETFE: −310°F to 311°F (−190°C to 155°C)
- PVDF: −40°F to 284°F (−40°C to 140°C)
A liner is not an automatic upgrade. It adds cost, lengthens lead time, and introduces bond-line and permeation considerations that a bare laminate does not have. It is the right answer when temperature, halogen acid permeation, or oxidizer strength puts the duty outside what the resin alone will hold.
Whatever resin is proposed, the supporting evidence should be chemical resistance data developed the way ASTM C581 describes — coupons of the actual resin system exposed to the actual reagent over time — rather than a generic compatibility chart. For liner materials, resistance to the reagent is evaluated under the practices in ASTM D543.
Vacuum Is the Design Case Most Often Omitted
This is the most common gap in scrubber inquiries. Fume control systems almost always run at negative pressure: the fan is downstream, pulling gas through the system. That means the duct, and frequently the absorber shell, are in vacuum service, and the governing failure mode is not corrosion — it is buckling.
A thin-wall FRP duct that is more than adequate for the chemistry will collapse under a modest negative pressure if it was never designed for it, and it will do so instantly rather than progressively. The design response is wall thickness plus external stiffening rings at a calculated spacing, and both depend on the design vacuum, not the normal operating vacuum.
The design vacuum should be the pressure the fan can develop against a fully blocked system, not the normal differential. A packing bed that fouls, a plugged mist eliminator, or a damper that closes without warning can take a duct to fan shut-off pressure in seconds. That number belongs in the inquiry; if nobody has calculated it, the fan curve is enough and we will calculate it.
The same logic applies to supports. FRP duct is light empty and heavy when full of condensate and fouling. Support spacing, hanger design, and slope to drain points are part of the scope, not a field decision.
What We Need in Order to Quote
- Gas flow rate, stated as actual or standard conditions
- Full gas composition with concentration ranges for each corrosive species, including trace oxidizers
- Inlet gas temperature: normal, maximum, and upset
- Dew point and expected condensate chemistry, if known
- Design vacuum or fan shut-off pressure, and design internal pressure if any
- Scrubbing liquor chemistry, concentration, and temperature
- Packing type, depth, and wet operating weight, if supplied by others
- Required removal efficiency and the emission limit behind it
- Wind, seismic, and snow criteria for the installation site
- Duct routing, support points, and available slope for condensate drainage
- Nozzles and access: inspection ports, manways, instrument connections, drain points
- Any flame spread requirement the installation must satisfy
- Exterior finish, UV protection, and whether a conductive or grounded interior surface is required
The last two are the most frequently omitted and the ones that generate the most change orders. Flame spread requirements in particular change the resin family available, so they need to appear in the inquiry rather than in the approval drawing review.
How We Verify the Work
Cylindrical sections — absorber shells and straight duct runs — are filament wound to ASTM D3299, where winding gives better and more repeatable structural properties. Hoods, transitions, hoppers, fittings, and any geometry that is not a simple cylinder are contact molded to ASTM D4097.
Quality control on the finished laminate includes thickness verification, visual inspection of the corrosion barrier against the acceptance criteria of the applicable standard, and Barcol hardness per ASTM D2583 as a cure check. Chemical resistance of the resin system is supported with data developed under ASTM C581.
One important point: a scrubber operating at atmospheric pressure or under fan-induced vacuum is not a pressure vessel. Specifying it as one adds cost without adding protection. Pressure vessel codes belong in the specification only when the equipment is genuinely designed for internal pressure.
Our Experience
We have been manufacturing FRP exclusively for more than 40 years, across more than 2,600 projects in mining, chemical processing, and water and wastewater treatment. Fume control systems have been a steady part of that work, and the pattern in the equipment we are asked to replace is consistent: the resin was usually adequate, and the problem was somewhere else — an outlet duct with no drainage slope that held condensate against the wall, a stiffening ring layout designed for operating vacuum instead of shut-off vacuum, or a hot inlet that was never quenched to the temperature the laminate was built for.
We have also been applying fluoropolymer liners for more than 20 years, which gives us a practical view of when a liner earns its cost and when a properly selected bare laminate will do the same job for less. That conversation is worth having before the design is frozen, not after.
Conclusion
FRP is the right material for most acid fume control duty, and it has the service record to prove it. But a scrubber is a system, not a vessel, and the parts that fail are usually the parts nobody specified: the vacuum case, the drainage, the transition between temperature zones. Send the full gas and vacuum data with the inquiry, ask for a laminate schedule broken out by zone, and require D4097, D3299, and C581 in the purchase order.
If you are specifying a new scrubber, replacing a duct run that did not last, or working out whether your service needs a liner, send us the gas data and the fan curve. We will tell you what the laminate needs to be and what it does not.
Request a quote from Plastimarmol FRP
References
ASTM International. (2022). Standard practice for determining chemical resistance of thermosetting resins used in glass-fiber-reinforced structures intended for liquid service (ASTM C581-22). ASTM International.
ASTM International. (2023). Standard specification for filament-wound fiberglass-reinforced thermoset-resin corrosion-resistant tanks (ASTM D3299-16(2023)). ASTM International.
ASTM International. (2022). Standard specification for contact-molded glass-fiber-reinforced thermoset resin corrosion-resistant tanks (ASTM D4097-17(2022)). ASTM International.
ASTM International. (2021). Standard practices for evaluating the resistance of plastics to chemical reagents (ASTM D543-21). ASTM International.